

Our New Website is Live – More Clarity, Quicker Access to Information
13. February 2026
Blocked Stock & Quarantine: Preventing Mixing Reliably
11. May 2026
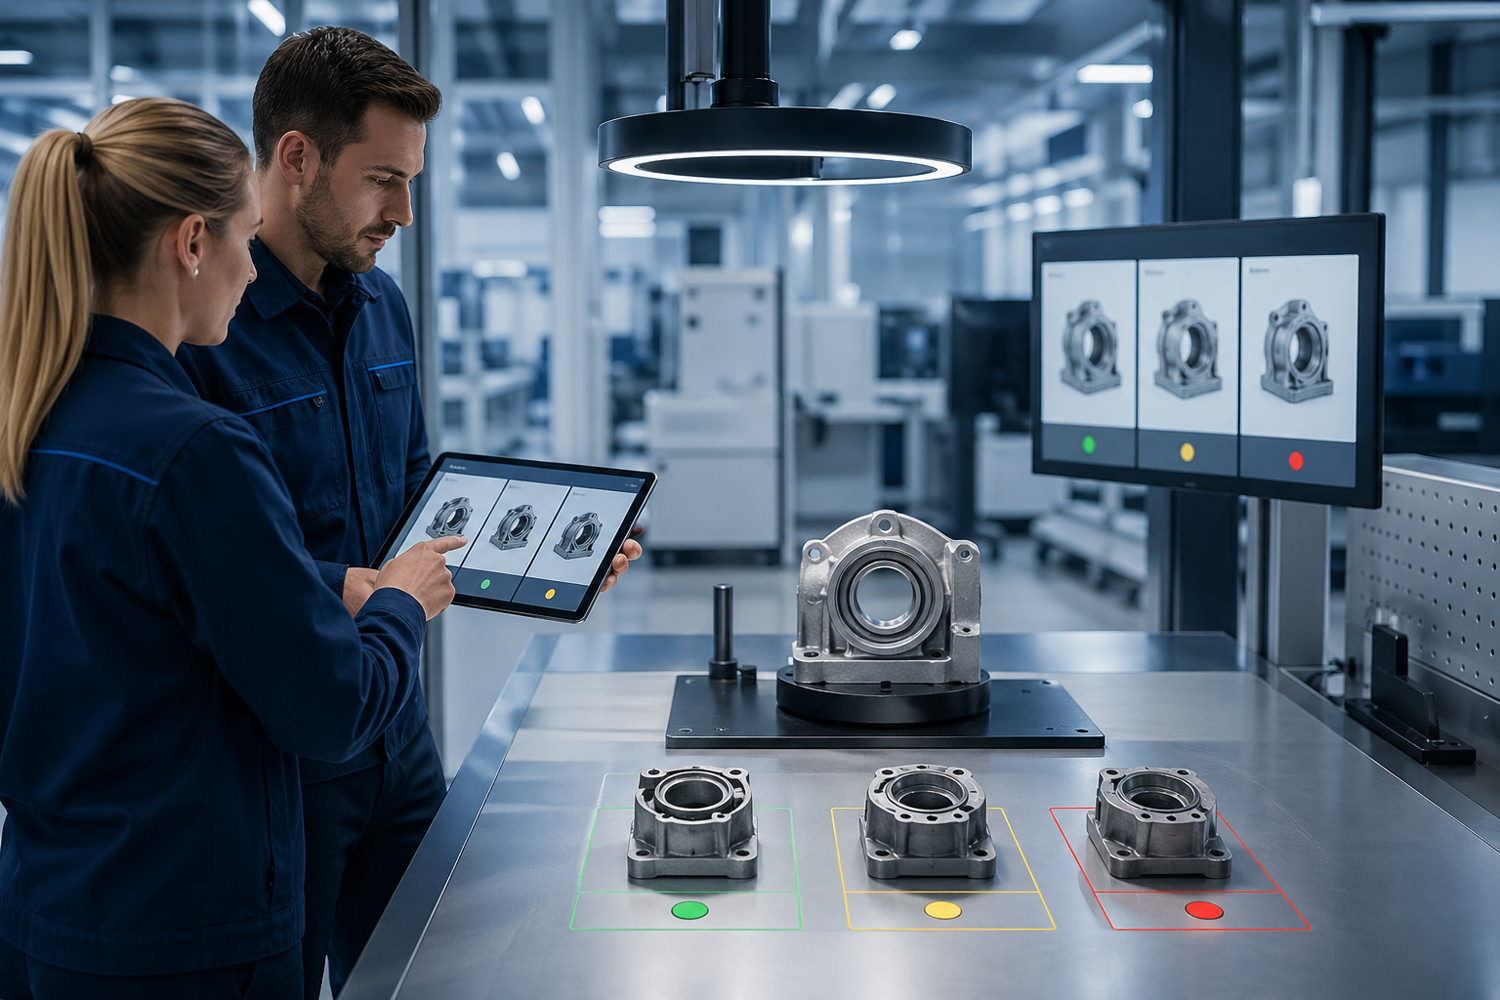
The images on this website were created using artificial intelligence (AI).
If two inspectors check the same part and reach two different results, you don't have a personnel problem. You have a standards problem. This is exactly where the defect catalog and boundary samples come in. They make quality measurable, repeatable, and defensible. And they prevent what eats up the most time and money in practice: discussions, re-inspections, unnecessary sorting actions, and complaints because "everyone saw it differently."
A clean defect catalog plus boundary samples is one of the strongest levers for achieving stable inspection processes. Regardless of shift, location, or person.
What a Defect Catalog Truly Achieves
A defect catalog is not a "photo album." It is a shared understanding of:
-
Which defect patterns exist?
-
What do they look like?
-
Where do they typically occur?
-
At what point is a part NOK?
-
What constitutes a borderline case?
In this way, it reduces the room for interpretation. This is exactly what makes inspections faster and more stable.
Boundary Samples: The Game Changer Against "Gut Feeling"
Boundary samples are real or referenced parts that show the transition between OK and NOK. They are so valuable because they end discussions in seconds:
-
"This is what OK looks like."
-
"This is what NOK looks like."
-
"And this here is the limit."
Especially for visual characteristics (surface, scratches, paint, burrs, warpage), boundary samples are often more important than any written description.
Step 1: Start with the 10 Most Common Defect Patterns
Many build defect catalogs that are too large and too complicated. Better: start small, but clean.
Take the defect patterns that really cause pain:
-
the most common reasons for complaints
-
the most expensive rework
-
the defects that slip through most often
-
the defects that trigger the most discussion
Once these top issues are standardized, the effort pays off immediately.
Step 2: A Structure That Everyone Understands Immediately
A practical defect catalog doesn't need novels. It needs a clear, recurring structure for each defect pattern. The following has proven effective:
-
Defect name (unique, short)
-
Description: what exactly is it (not "bad," but specific)
-
Typical location on the component: where to find it
-
Identifying feature: what it looks like, how to recognize it reliably
-
OK/NOK differentiation: clear decision
-
Borderline case rule: what to do in case of uncertainty (e.g., second inspection / QA decides)
-
Example images: OK, limit, NOK (same light/same perspective)
-
Inspection environment note: light, distance, aids (magnifying glass, inspection lamp, ring light)
This allows every inspector to work immediately without having to interpret first.
Step 3: Standardize the Inspection Environment, Otherwise Images Are Useless
A defect catalog is only as good as the inspection situation. If inspections are carried out under good lighting during the day shift and in a dark corner at night, the result will inevitably differ.
Therefore: define the basics.
-
same light source or defined inspection station
-
defined viewing distance
-
defined inspection duration per part (realistic, not theoretical)
-
defined aids
This is not overengineering. This is the prerequisite for a standard to work at all.
Step 4: Select and Maintain Boundary Samples Properly
Boundary samples are not "just any broken part." They must be representative and show exactly the limit that will be decided later.
Important points:
-
Prefer real parts (if possible), because photos can be deceptive.
-
Multiple boundary samples per defect pattern if the variance is high.
-
Protection and storage: boundary samples must not be damaged themselves.
-
Versioning: if customer/criteria change, boundary samples must be updated.
-
Access: boundary samples must be where the inspection takes place – not somewhere in the office.
A boundary sample that no one can find is useless.
Step 5: Rules for Borderline Cases – Otherwise It Will Slip Again
The most dangerous area is the borderline case. If there is no rule for it, gut feeling decides again.
A simple and effective rule:
-
Borderline case = second inspection (four-eyes principle) or QA approval
-
Borderline case is documented (to see if criteria are appropriate)
-
In case of frequent borderline cases: sharpen criteria or check the process
This prevents inspectors from "waving through" borderline cases due to time pressure.
Step 6: Training – Short but Mandatory
You don't need seminars. You need a short, recurring briefing that actually takes place. Especially for new inspectors, new defect patterns, or after customer feedback.
Proven methods:
-
10–15 minutes of instruction at the inspection station
-
show OK, limit, and NOK once
-
inspect a few parts together
-
clear question: "What do you do if you are unsure?"
This ensures the topic is practically anchored.
Typical Mistakes During Setup (and How to Avoid Them)
Too theoretical: long texts, few clear images, no real limit.
Too large: 100 defect patterns, but none are clean.
Without maintenance: criteria change, catalog remains old.
Without inspection environment: same images, but different lighting conditions, result shifts.
Without borderline case rule: everything becomes a matter of interpretation again.
If you avoid these points, the catalog will quickly become a real productivity tool.
Conclusion: A Standard Saves More Time Than It Costs
Defect catalogs and boundary samples are an investment that works immediately: less discussion, more stable inspection results, fewer re-inspections, and better communication with customers and internally.